Custom Rubber Extrusions China Manufacturer And Supplier
Seashore is a reliable manufacturer and supplier of custom rubber extensions, precision-extruded profiles, and bespoke sealing solutions trusted by engineers across automotive, construction, marine, and industrial sectors. From concept to continuous production, we engineer every profile to your exact dimensions, compound, and performance requirement — delivering consistent quality at scale, anywhere in the world.
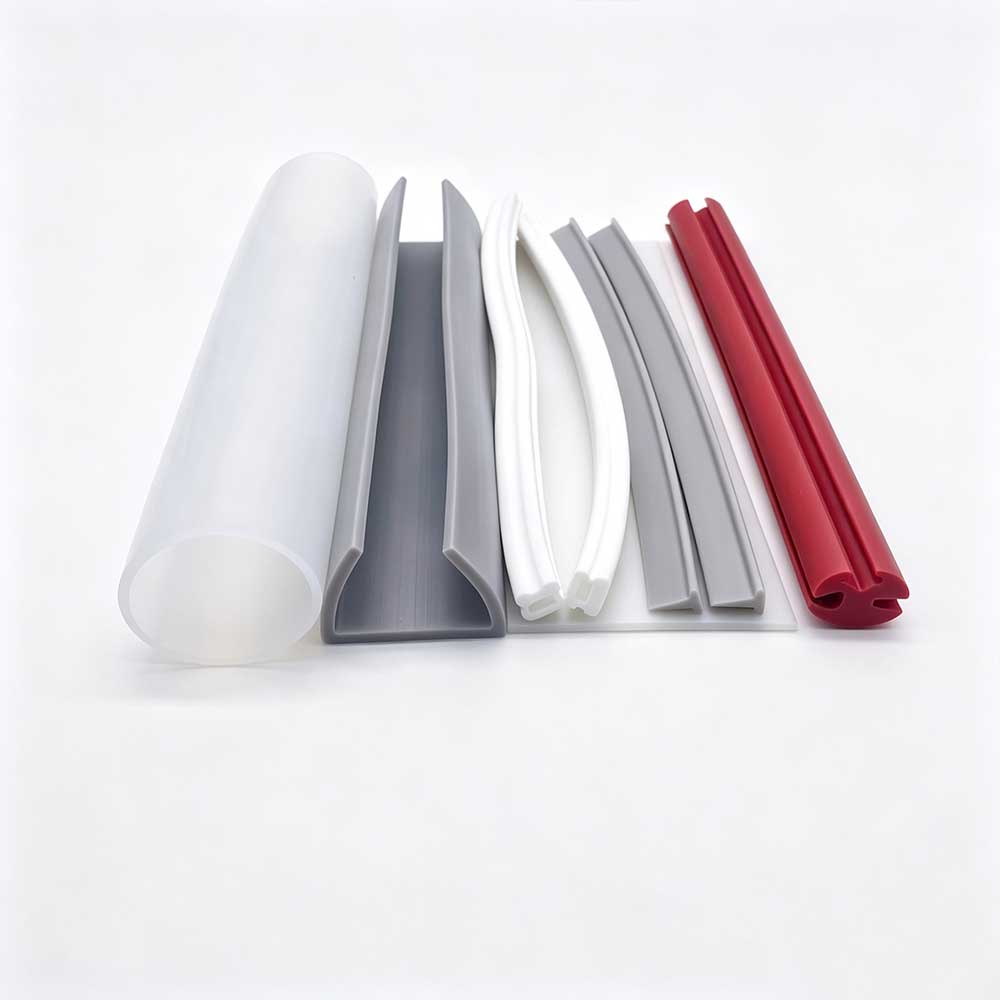
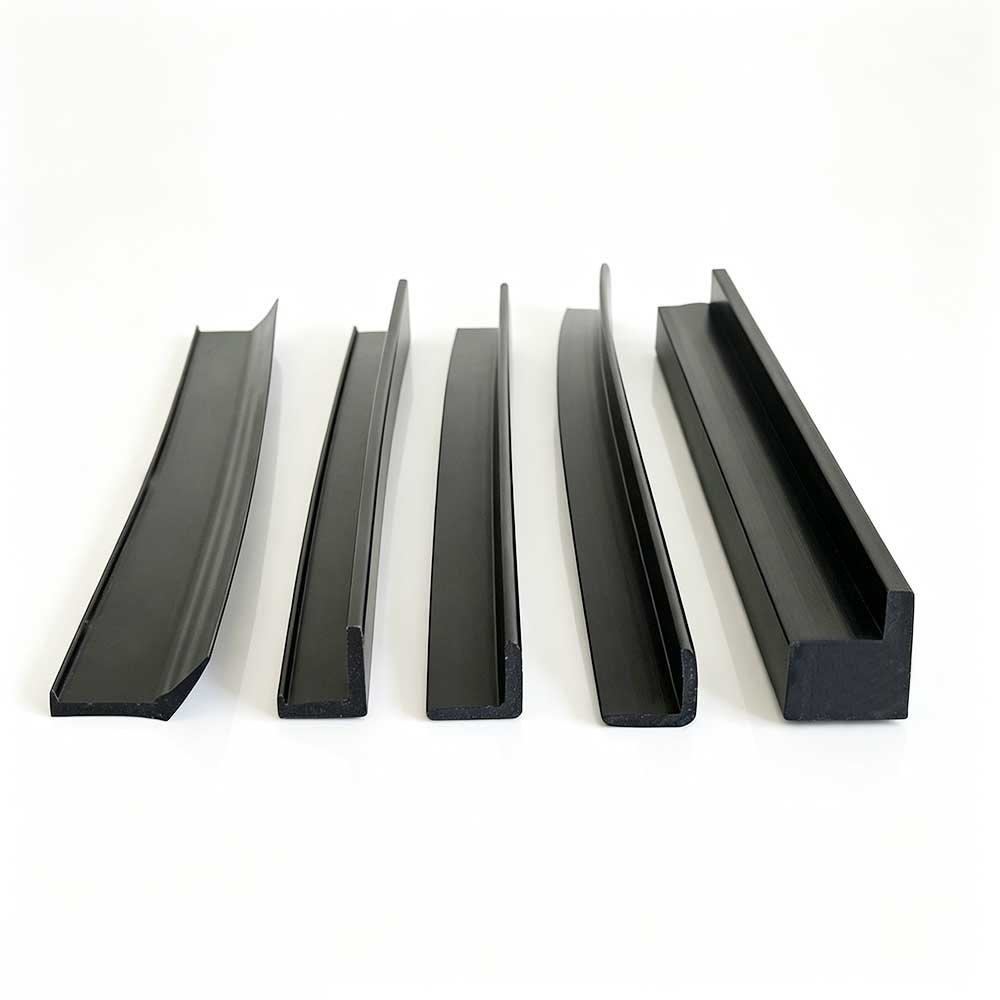

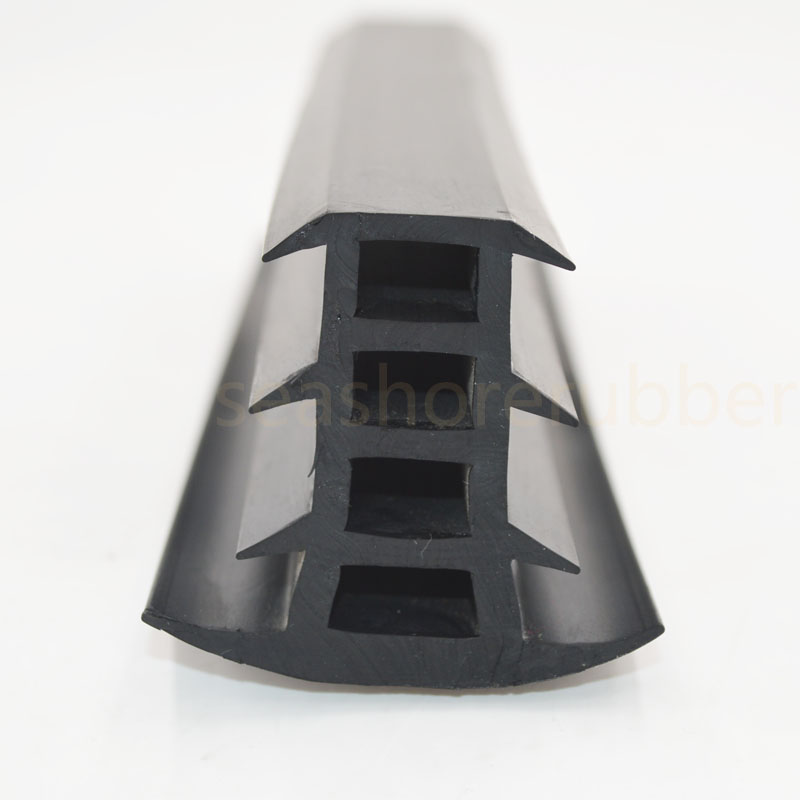
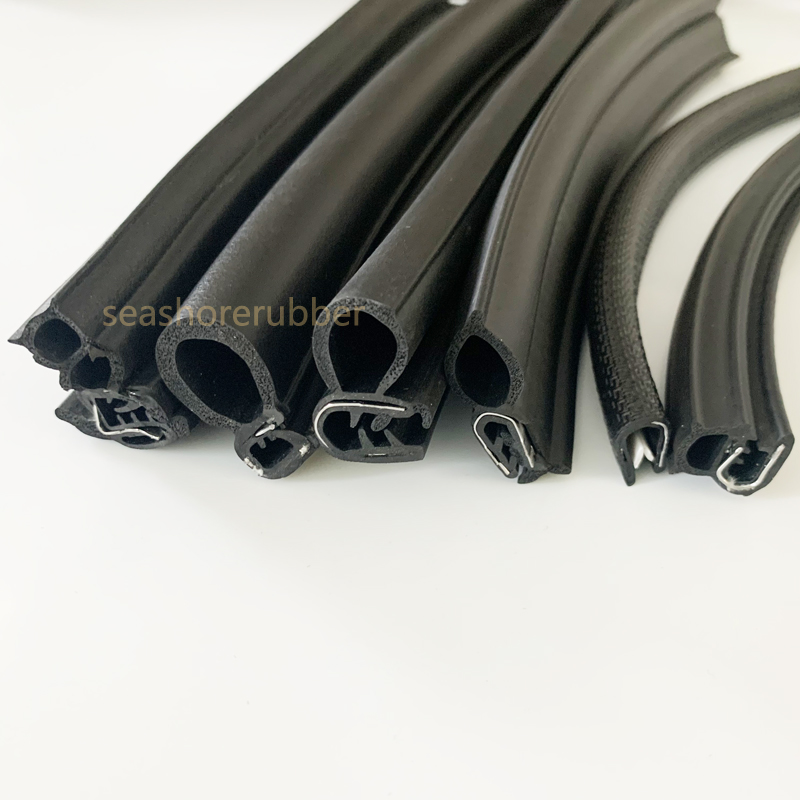
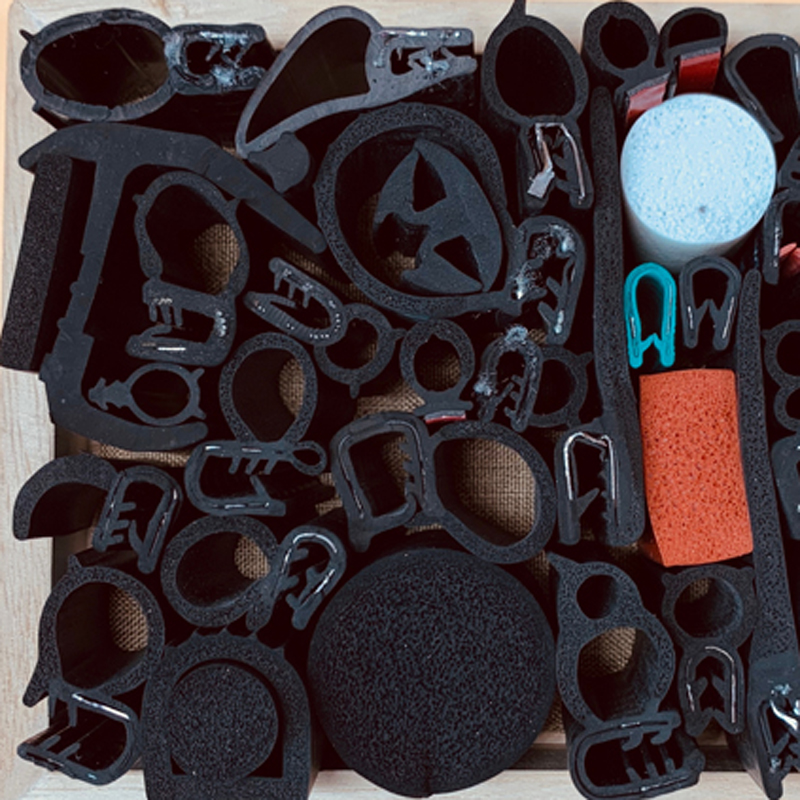
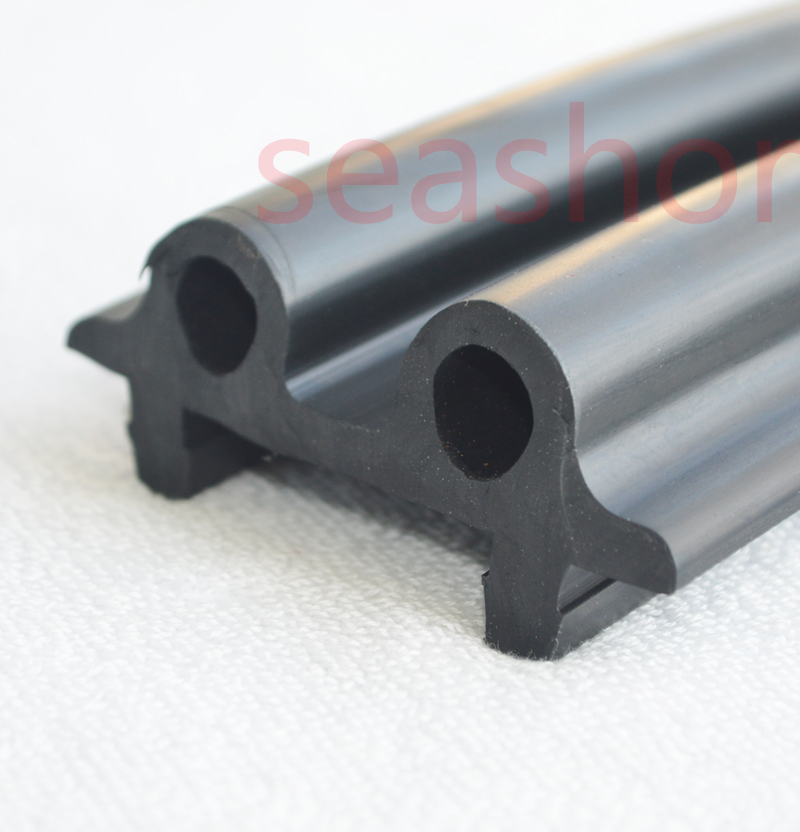 rubber gate seal
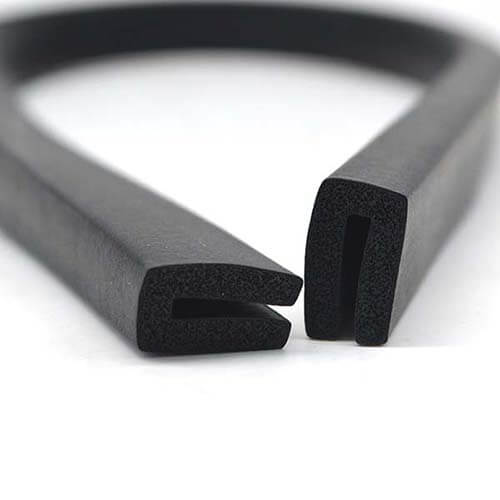 U Type Sponge Rubber (3)
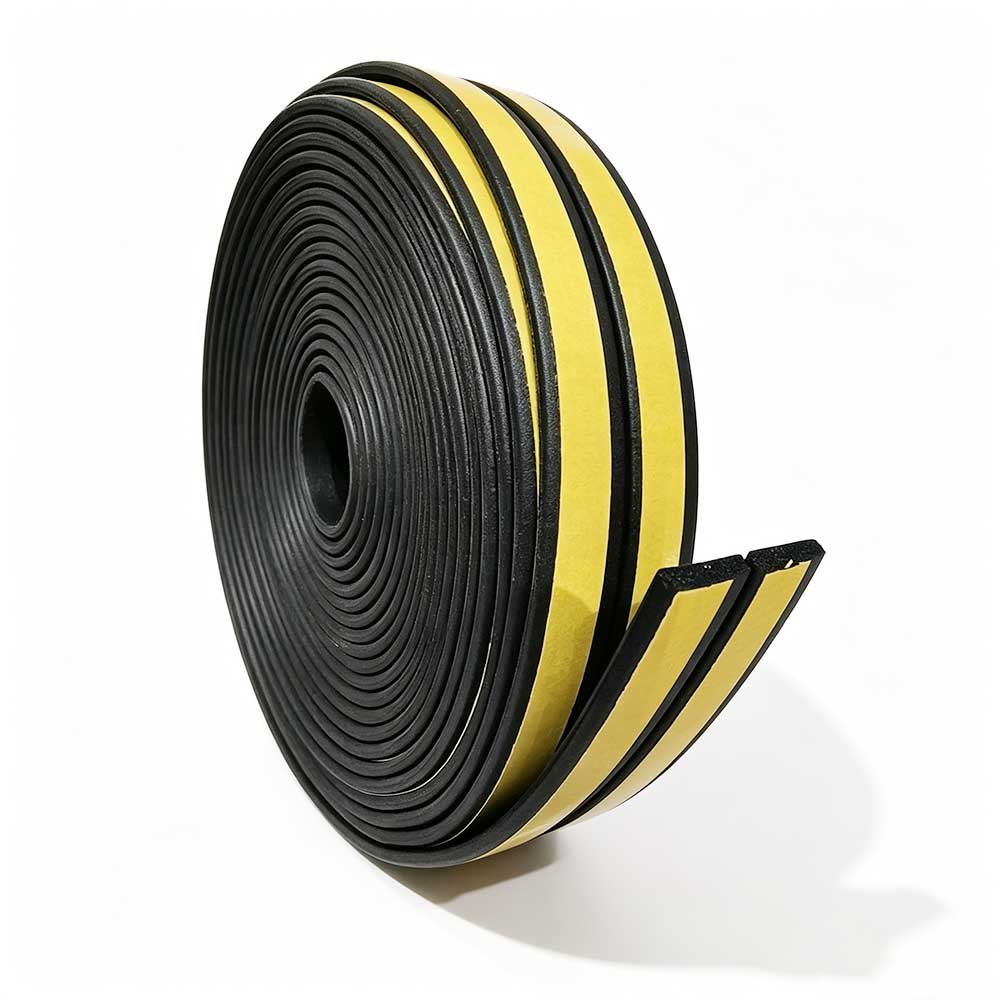
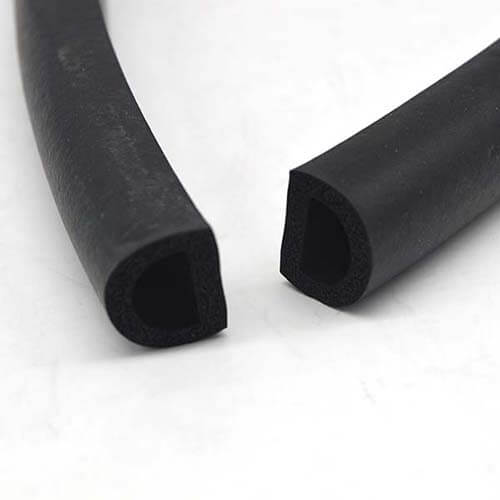 D Type EPDM Sponge Strip Seal (3)
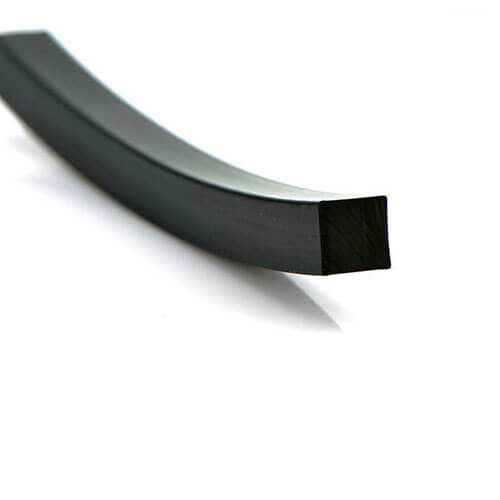 Epdm Rubber Square Cord Strip extrusion (2)
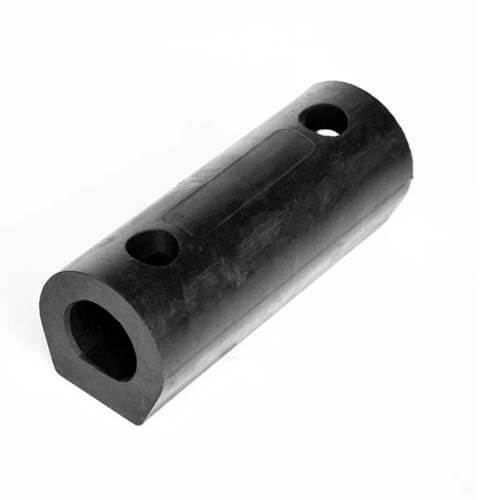 Extruded rubber D shape fender for marine (4)
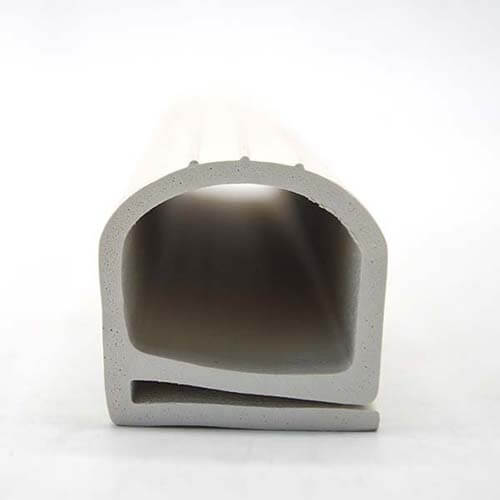 E Shape EPDM Rubber Seal For Cool Room Door (1)
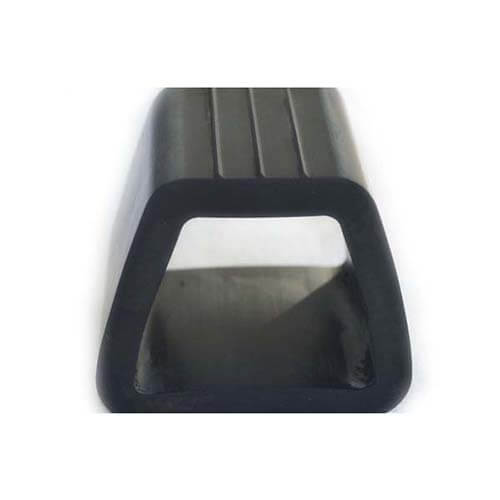 D Shape Fender EPDM Rubber (1)
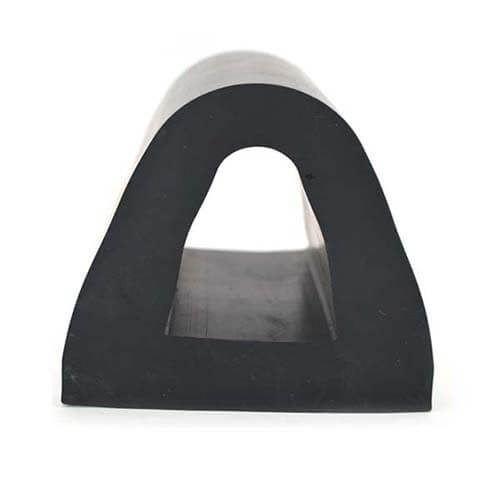 EPDM Rubber Marine Fender extrusion (3)
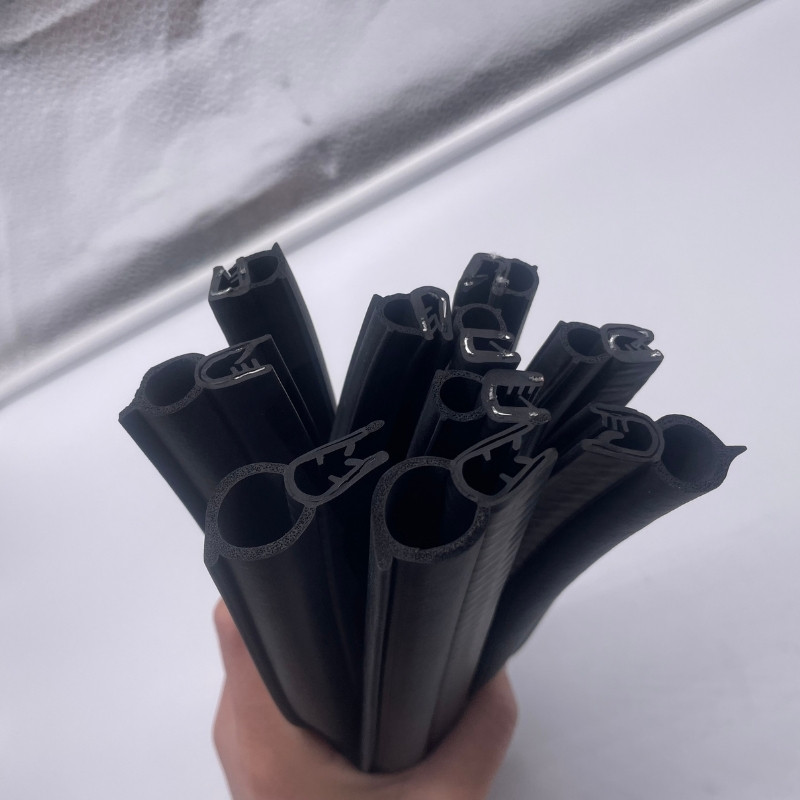
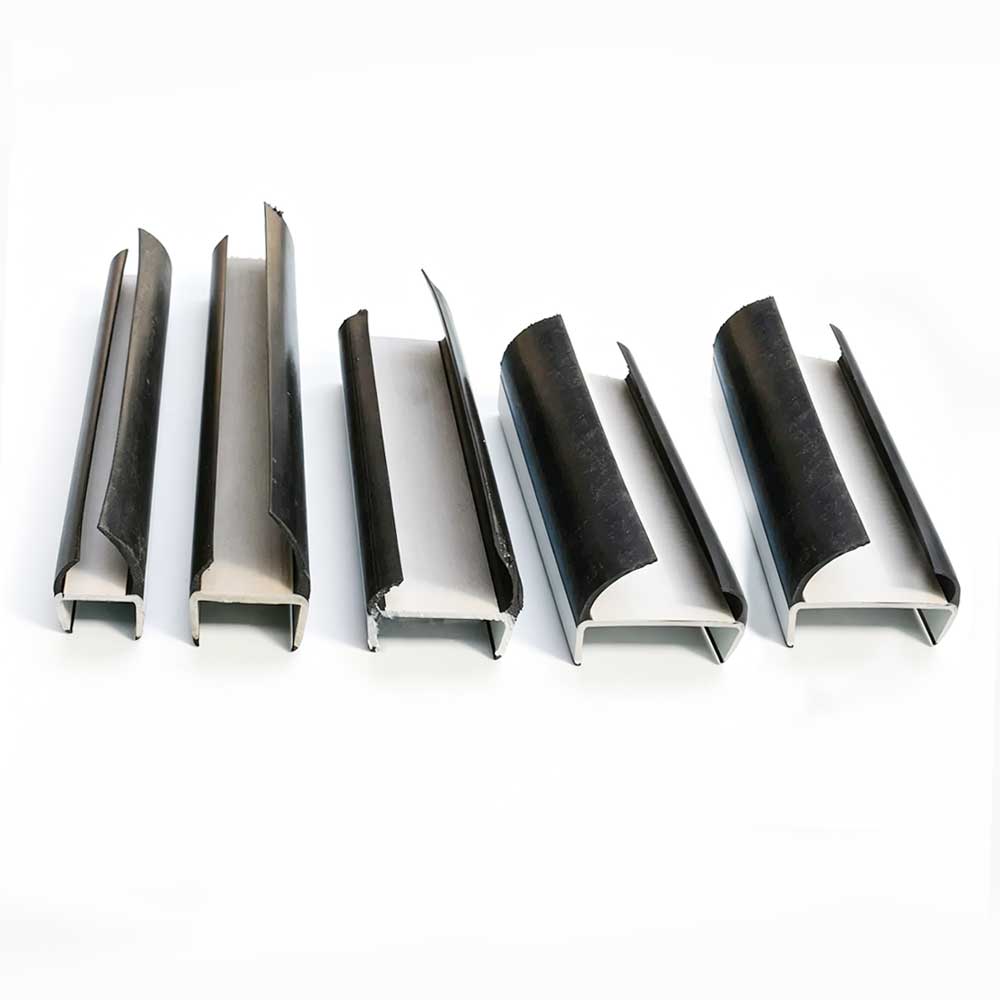
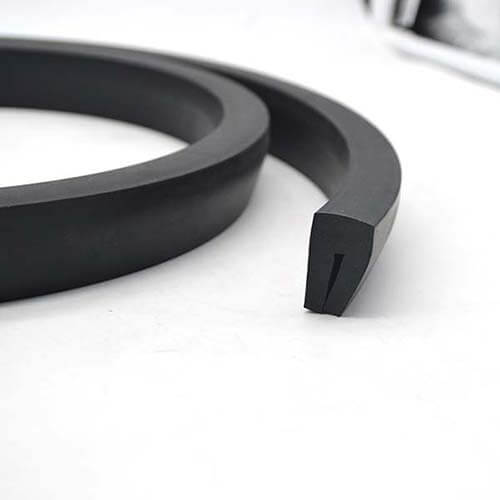 U Section EPDM Rubber Edge Seal (4)
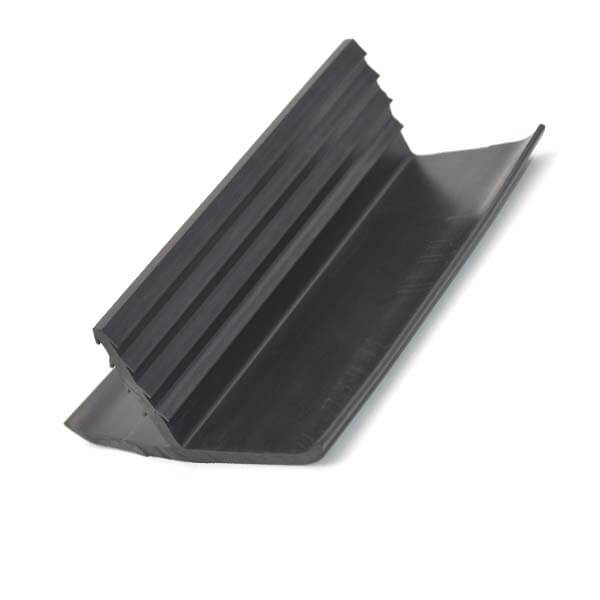 EPDM T Type profile Rubber For Truck Scale
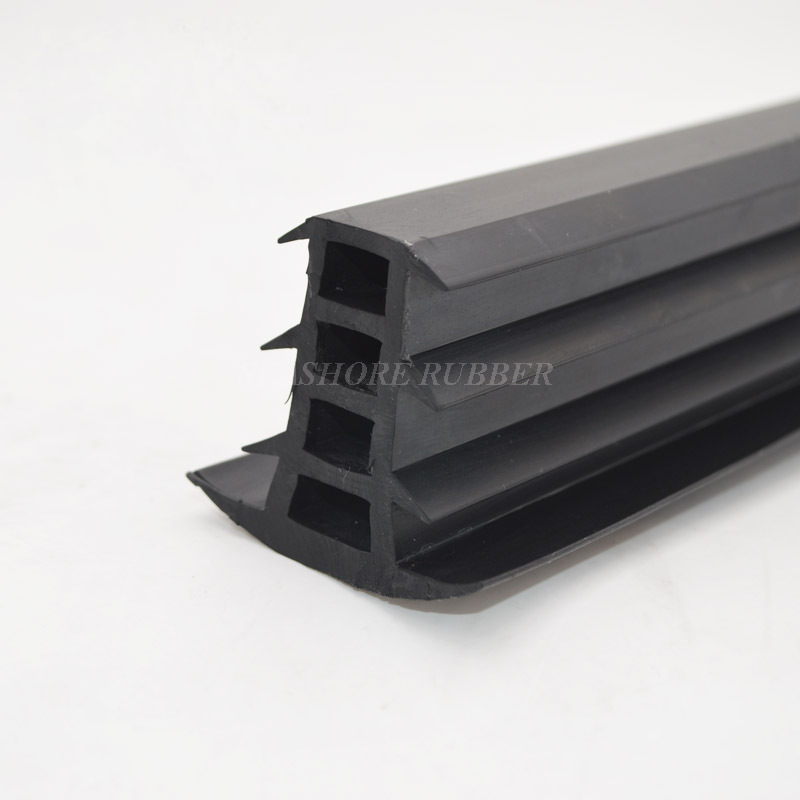

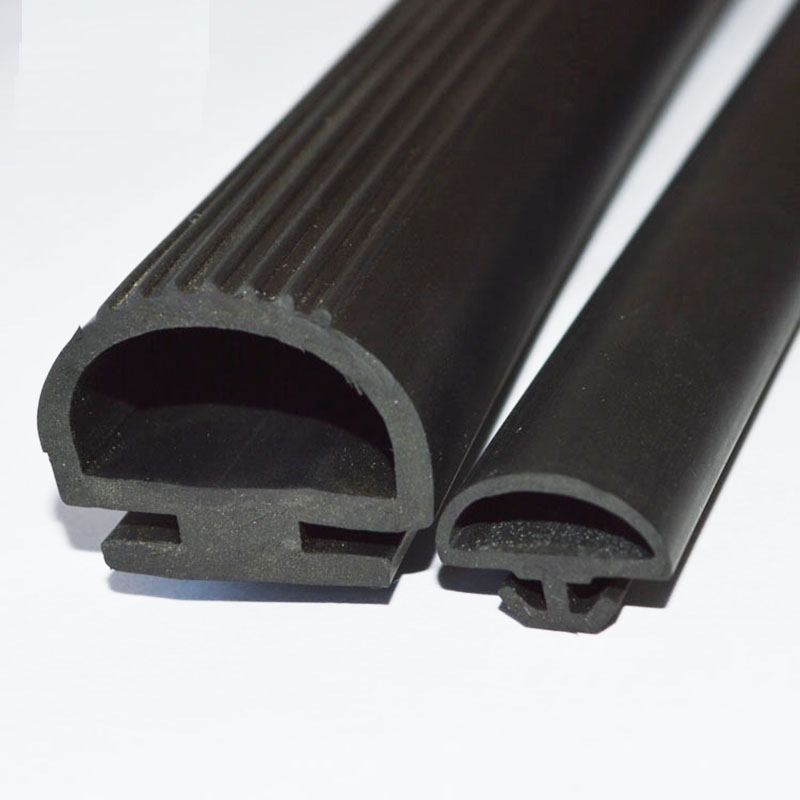
What Are Rubber Extrusions?
Custom rubber extensions are produced from customer-supplied drawings, CAD files, or physical samples to match exact dimensions and performance requirements. These products are widely used across sectors including automotive, aerospace, construction, food processing, marine, and industrial manufacturing.
Types of Custom Rubber Extrusions
Extruded Rubber Profiles
Continuous lengths with a consistent cross-section — ideal for seals, gaskets, and edge trims.
Rubber Cord Extrusions
Round or square cords cut to length; used in O-ring grooves, dynamic seals, and compression joints.
Sponge Rubber Strips
Closed or open-cell foam profiles for low-compression weatherstripping and acoustic damping.
Co-extruded Profiles
Dual-durometer extensions combining rigid and flexible rubber in a single piece for complex assemblies.
Rubber Channel Trim
U-channel or H-channel profiles that grip panel edges for protection and a finished appearance.
Bulb Seal Extrusions
Hollow bulb attached to a mounting base — standard for door, hatch, and enclosure sealing.
Key Materials for Rubber Extrusions
Material selection is the most critical decision. Each rubber compound has a unique performance envelope defined by temperature range, chemical resistance, UV stability, and compression set.
Ethylene Propylene Diene (EPDM)
The workhorse for outdoor, construction, and automotive applications. Excellent UV, ozone, water, and steam resistance. Long service life outdoors.
–40°C to +120°C · Most widely specified
Silicone Rubber (VMQ)
Unmatched thermal range. FDA-compliant grades for food and medical. Odourless, non-toxic, colour-stable. Higher cost but premium durability.
–60°C to +230°C · Food & medical grade
Neoprene – Chloroprene (CR)
Balanced profile — moderate oil resistance, good weathering, solid mechanical strength. Marine, HVAC, and electrical panel applications.
–40°C to +100°C · Marine-grade
Nitrile (NBR)
The standard for petroleum oils, fuels, and hydraulic fluids. Automotive fuel systems, hydraulic seals, pump gaskets. Poor UV resistance.
–35°C to +100°C · Oil & fuel resistant
Natural Rubber (NR)
Superior rebound resilience and fatigue resistance. Conveyor belts, anti-vibration mounts, agricultural seals. Poor ozone and oil resistance.
–50°C to +80°C · High fatigue life
Styrene-Butadiene (SBR)
Cost-effective general-purpose compound. Abrasion resistant. Used in flooring strips, conveyor profiles, and non-critical seals.
–40°C to +100°C · General purpose
Applications by Industry
Automotive Door and window seals, weatherstripping, trunk seals, hood and sunroof gaskets, glass run channels, noise and vibration dampening strips, radiator hose profiles, and underbody protective edging.
Construction & Architecture Window and curtain wall glazing seals, door perimeter seals, expansion joint covers, roofing edge trim, concrete form seals, flooring edge profiles, and structural glazing gaskets.
Aerospace & Defense Cockpit and fuselage door seals, access panel gaskets, environmental and pressure seals, vibration isolation mounts, fuel-resistant tubing profiles, and EMI/RFI shielding seals.
Marine Hatch and porthole seals, deck drain profiles, hull fender strips, watertight door gaskets, navigation equipment seals, and anti-slip deck edging.
Medical & Pharmaceutical Fluid transfer tubing, cleanroom door seals, equipment gaskets, sterilization-resistant profiles, lab instrument seals, and FDA-compliant food and drug contact profiles.
Industrial Manufacturing Machine guarding edge trim, conveyor belt edging, press and panel seals, access door gaskets, vibration dampening pads, tank and vessel seals, and cable management grommets.
Rail & Transportation Passenger door and window seals, inter-carriage gangway profiles, underframe seals, driver cab gaskets, luggage compartment seals, and exterior body panel trim.
Electronics & Electrical Enclosure and cabinet seals, EMI/RFI gaskets, waterproof panel seals, LED lighting channel profiles, switchgear gaskets, and outdoor junction box seals.
Food & Beverage FDA-approved conveyor seals, oven door gaskets, refrigeration unit seals, hygienic equipment profiles, food processing machine seals, and cold storage door strips.
Renewable Energy Solar panel frame seals, wind turbine nacelle gaskets, battery enclosure seals, inverter cabinet profiles, offshore platform seals, and weatherproof junction box gaskets.
Rubber Extrusion Manufacturing Process
Compound Preparation
The manufacturer prepares compounds containing the base polymer, reinforcing fillers, processing aids, curing ingredients, and other additives.
Consistent mixing matters because changes in compound behavior can affect material flow, finished dimensions, and physical properties.
Extrusion Through Shaped Dies
Uncured rubber enters the extruder, where the rotating screw moves it toward the die. The die opening forms the continuous cross-sectional shape.
Rubber can expand after leaving the die, a behavior known as die swell. Tooling must account for this behavior rather than simply reproduce the finished drawing dimensions.
Curing and Cooling
The extruded section is cured through a process suited to its compound and geometry. Curing creates the cross-linked structure needed for elastic recovery and dimensional stability.
Process control must balance line speed, temperature, and curing time. Cooling and handling must also avoid stretching or deforming the profile.
Cutting and Secondary Processing
After curing, profiles may be supplied in coils, cut into lengths, or processed into finished assemblies. Available operations can include punching, notching, drilling, and other cutting methods. These features help adapt continuous extrusions to specific installation requirements.
Rubber Extrusion Profiles Selection Factors
Service Environment
Identify exposure to sunlight, ozone, water, oils, cleaning chemicals, heat, and cold. Include both normal operation and occasional maintenance conditions.
A seal may perform well during operation but degrade when exposed to incompatible cleaning agents.
Compression and Closing Force
Sealing requires sufficient contact pressure, but excessive compression can increase closing effort, distort the section, and accelerate permanent deformation.
There is no universal compression percentage for every rubber profile. Use recommendations for the specific section and verify them through assembly testing.
Mounting and Retention
Profiles may fit into grooves, grip edges, attach mechanically, or use adhesive backing. The mounting method must suit the substrate, vibration, temperature, and installation process.
Adhesive-backed seals also depend on surface cleanliness, adhesive compatibility, and application conditions. The rubber compound and adhesive system require separate evaluation.
Shape Recovery After Compression
Choose rubber profiles that can recover their shape after prolonged compression. Seals that remain flattened may lose contact with mating surfaces, allowing water or dust to enter.
Check compression set data under conditions relevant to the application, including temperature and compression duration. Rubber hardness alone does not indicate how well profiles will recover
FAQ
1. What is the difference between solid and sponge/foam rubber extrusions?
Solid rubber extrusions are made from dense, fully cured rubber and offer superior strength, abrasion resistance, and load-bearing capacity. Sponge or foam rubber extrusions contain a cellular (open or closed-cell) structure, making them lighter, more compressible, and better at conforming to irregular surfaces with low closure force. Sponge profiles are ideal for low-pressure sealing applications, while solid profiles suit higher-stress environments. Many assemblies use both — a sponge bulb seal with a solid mounting base, for example.
2. How are rubber extrusions joined frames and loops?
Straight lengths of rubber extrusion can be cut and joined end-to-end or formed into continuous frames (rectangles, circles, custom shapes) using several methods: vulcanized splicing (bonding with heat and adhesive for the strongest, most seamless joint), cold bonding (using contact cement — faster but less durable), and corner molding (molded rubber corners joined to straight extrusions for precise mitered frames). The best method depends on the performance requirements, profile geometry, and budget.
3. Can rubber extrusions be produced with co-extrusion?
Yes. Co-extrusion is a process where two different rubber compounds — or a rubber and a thermoplastic — are extruded simultaneously through a single die to produce a single integrated profile. This allows one profile to have, for example, a rigid mounting leg (high durometer/hardness) combined with a soft, flexible sealing lip (low durometer). This eliminates the need for assembly of separate parts and improves consistency, and is widely used in automotive weatherstripping and architectural glazing seals.
4. What rubber materials can be extruded?
Seashore Rubeer can provide extrusions in a wide range of rubber materials, including EPDM, CR, NBR, Natural Rubber, Silicone, HNBR, Viton, and SBR. We also offer plastic extrusions in PVC, TPE, and TPV.


